

Description
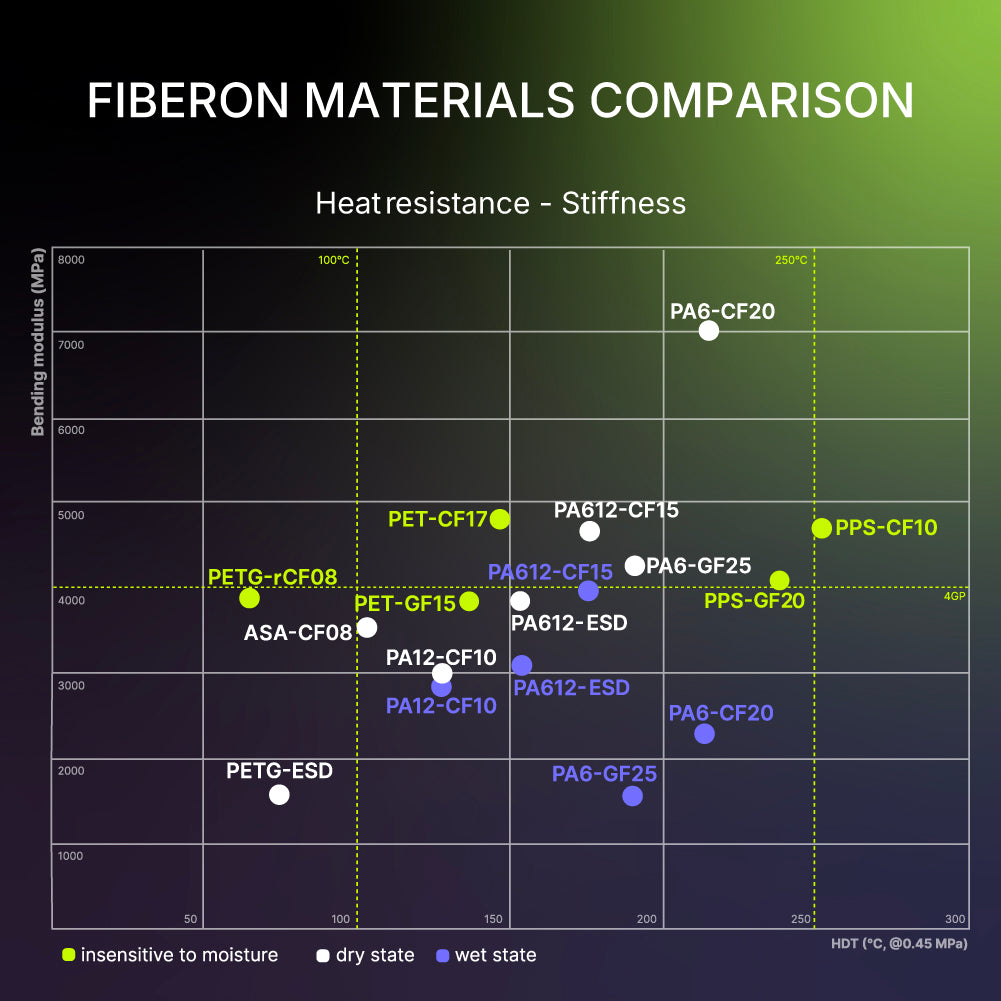
✓ High Strength & Stiffness
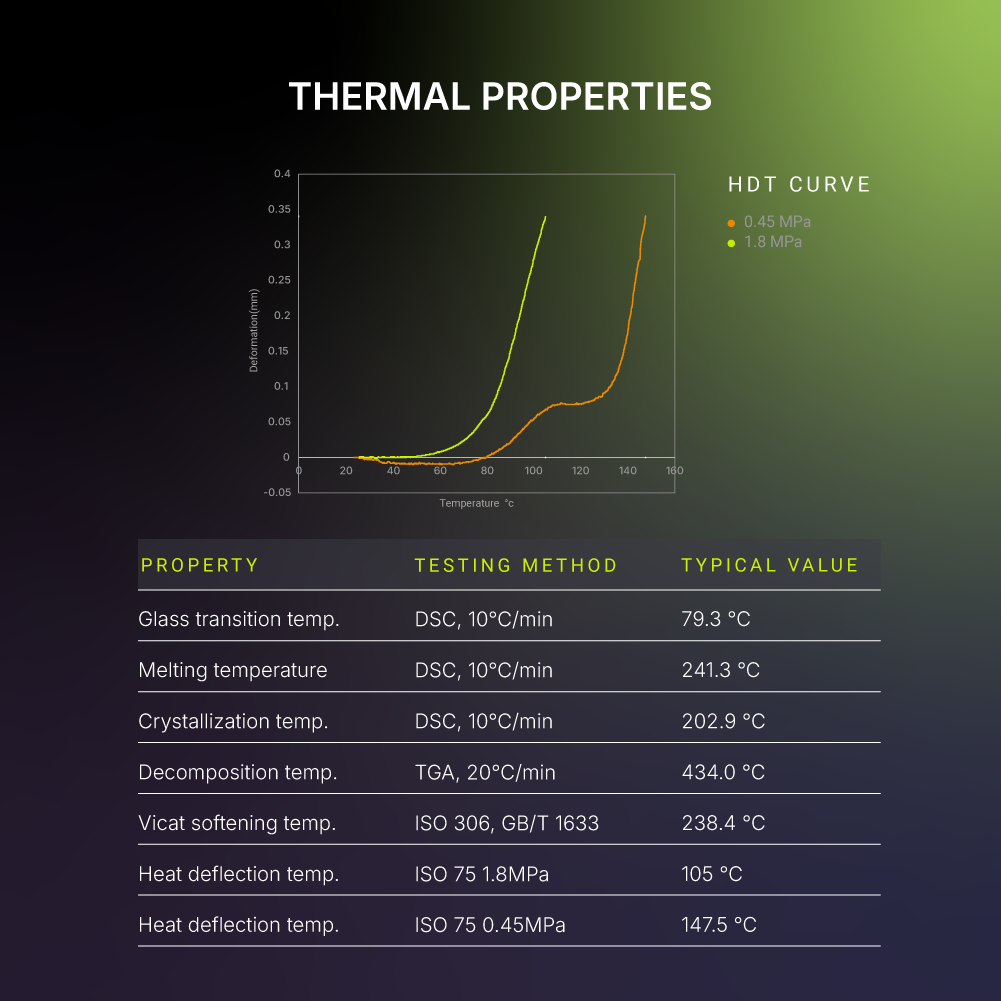
✓ High Heat Resistance
✓ Ready to Print
✓ Easy to Print
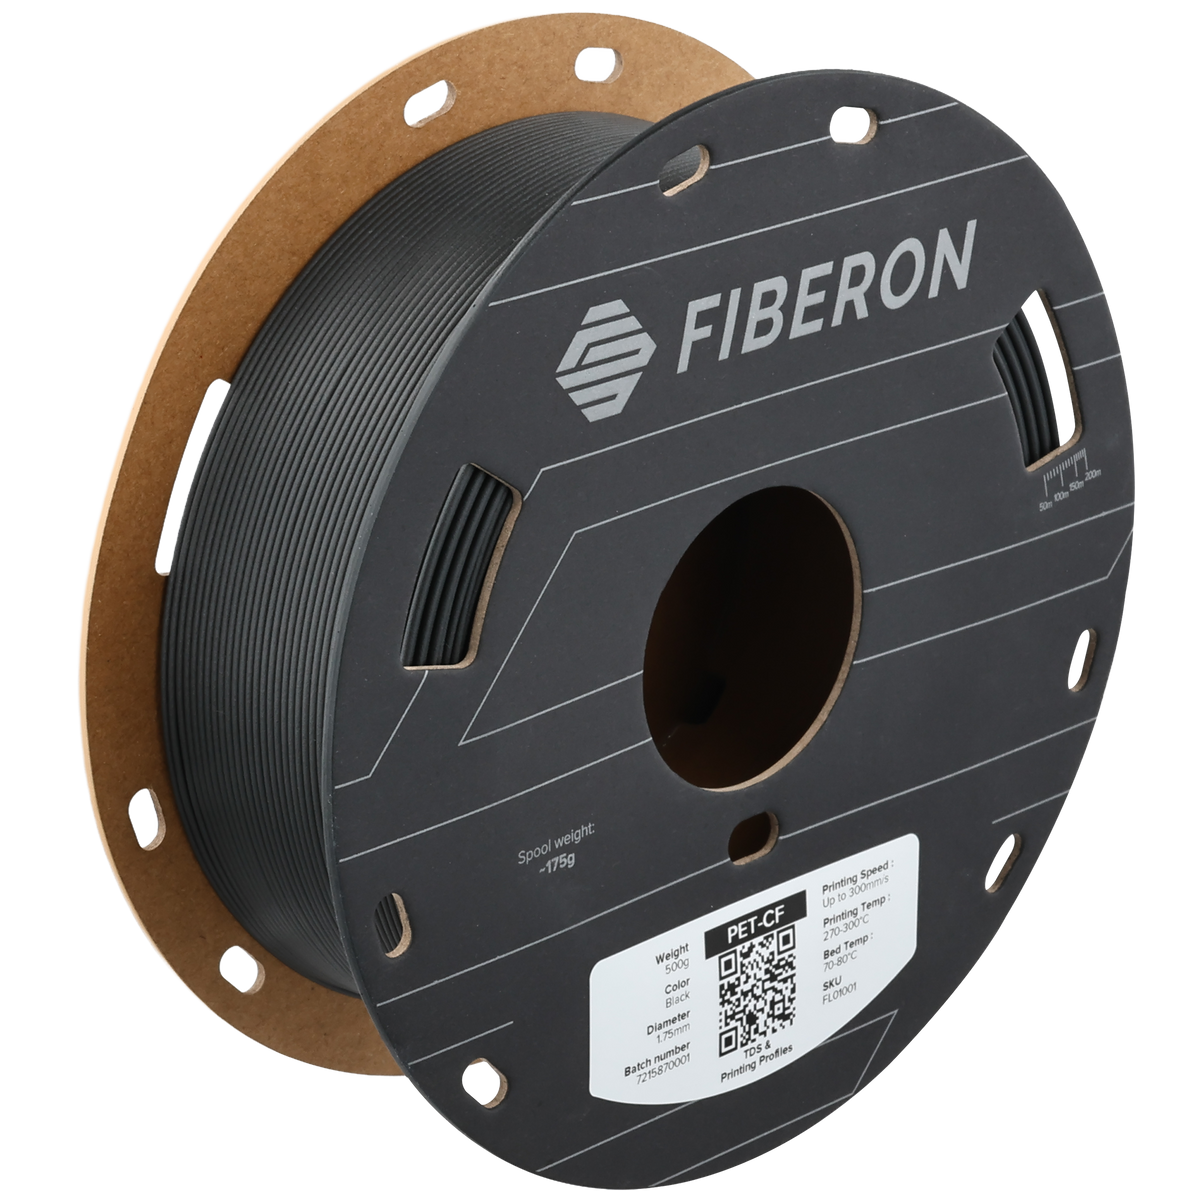
Fiberon™ PET-CF17: High-Performance Carbon Fiber Reinforced PET Filament
Engineered for Strength and Precision
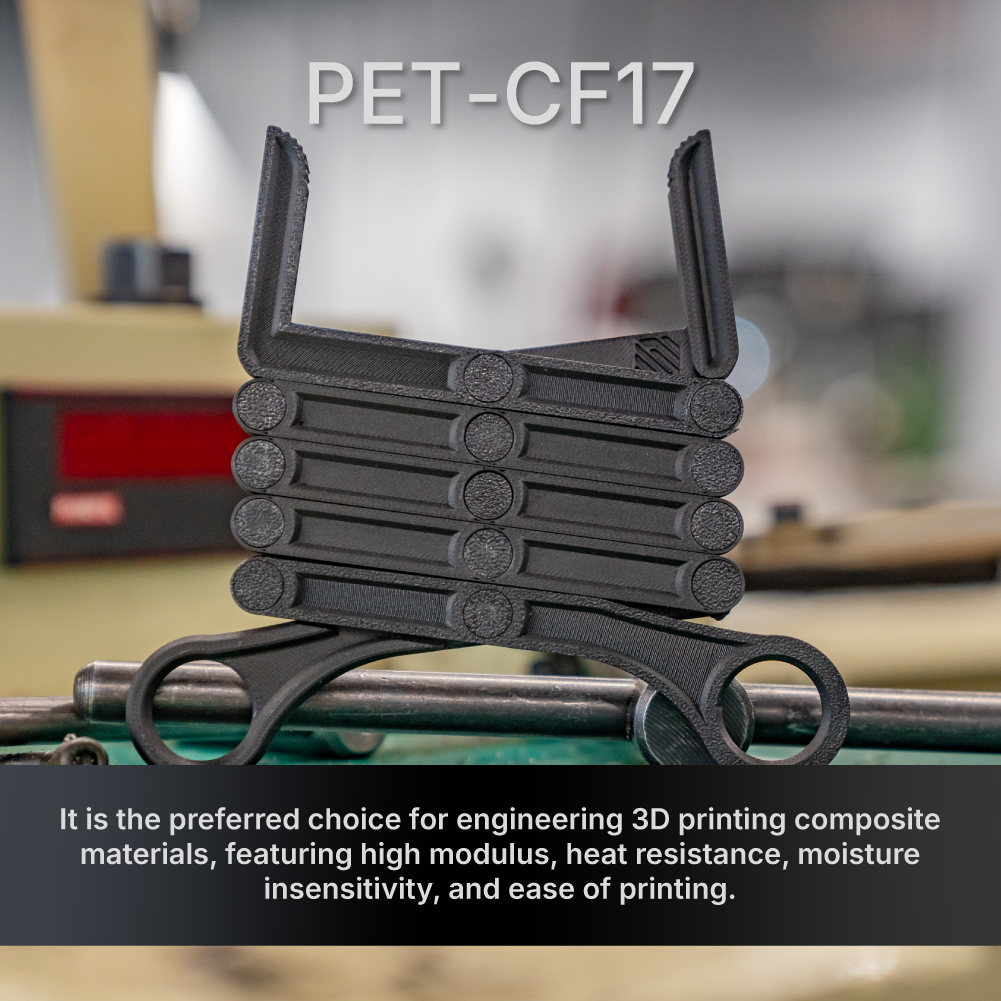
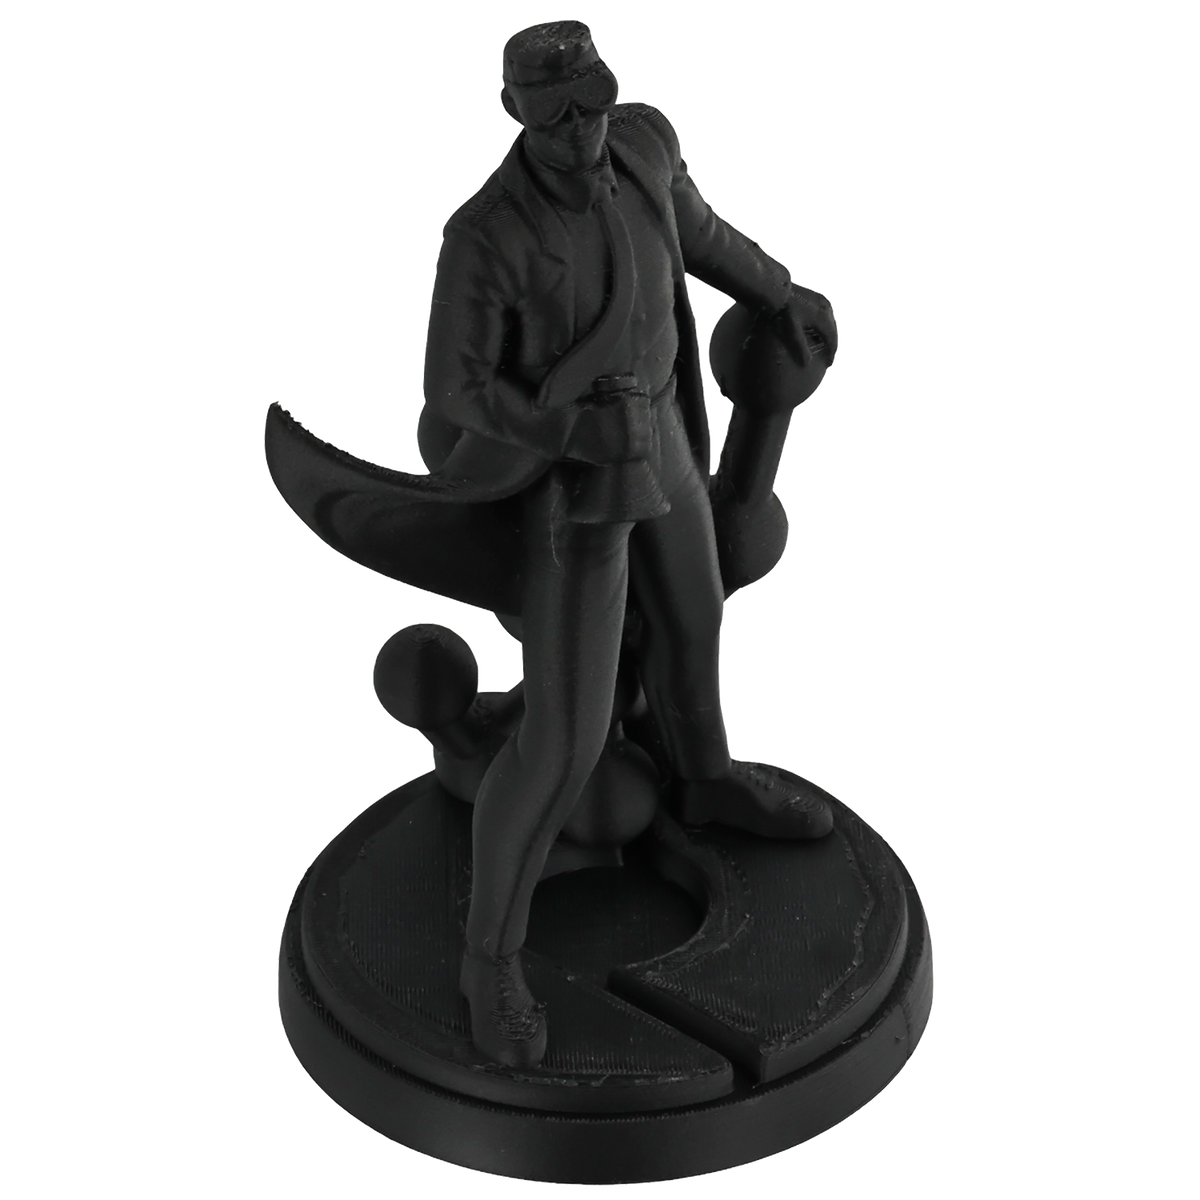
Fiberon™ PET-CF17 is a carbon fiber reinforced PET (polyethylene terephthalate) filament, specifically designed for engineering-grade 3D printing. With 17% carbon fiber content, it delivers a high modulus for excellent stiffness and dimensional stability, making it ideal for functional prototypes and end-use parts.
Key Performance Features
High Modulus & Strength: The carbon fiber reinforcement provides outstanding rigidity and mechanical strength, suitable for demanding engineering applications.
Heat Resistance: Maintains structural integrity at elevated temperatures, making it suitable for parts exposed to heat or requiring thermal stability. Annealing is required for higher heat resistance.
Moisture Insensitivity: Unlike many engineering filaments, Fiberon™ PET-CF17 is less sensitive to moisture, ensuring consistent print quality and reducing the need for pre-drying.
Easy to Print: Offers smooth extrusion and reliable bed adhesion, making it accessible to users with standard high-temperature FDM/FFF 3D printers equipped with a hardened nozzle.
Ideal for Engineering Applications
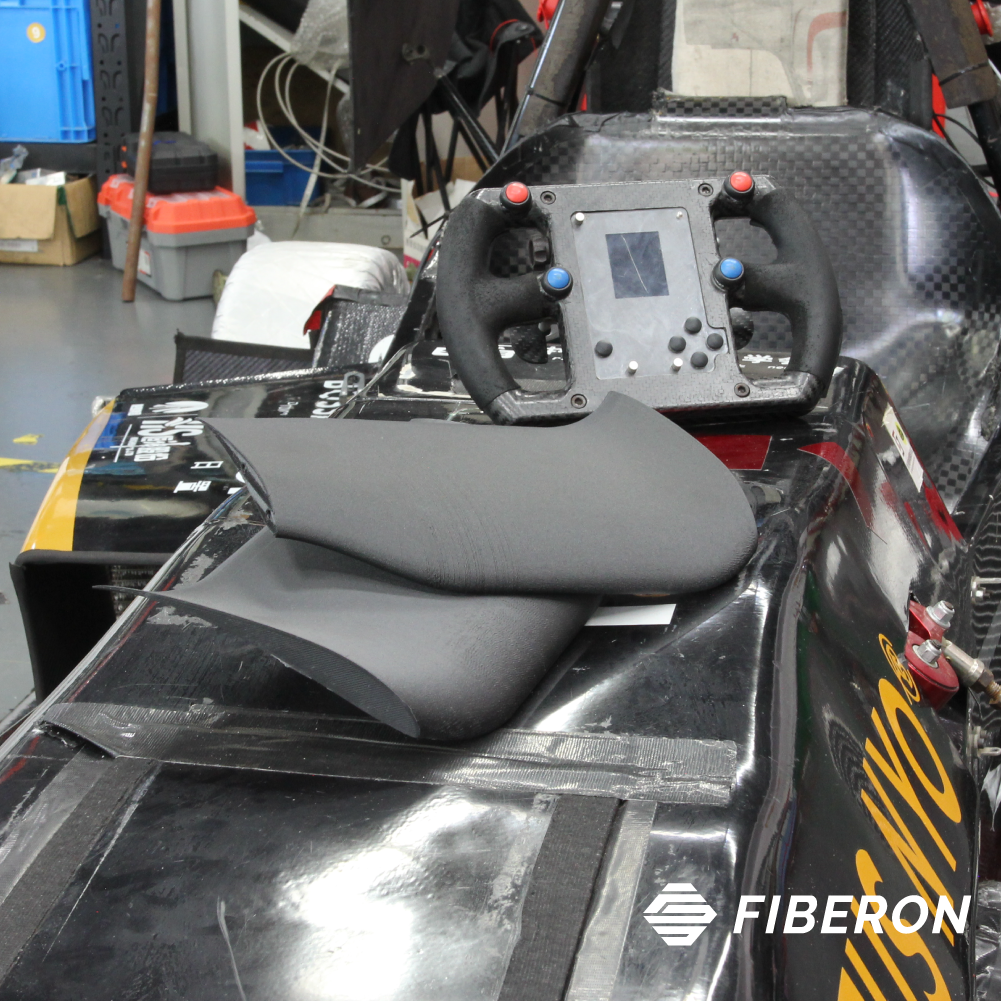
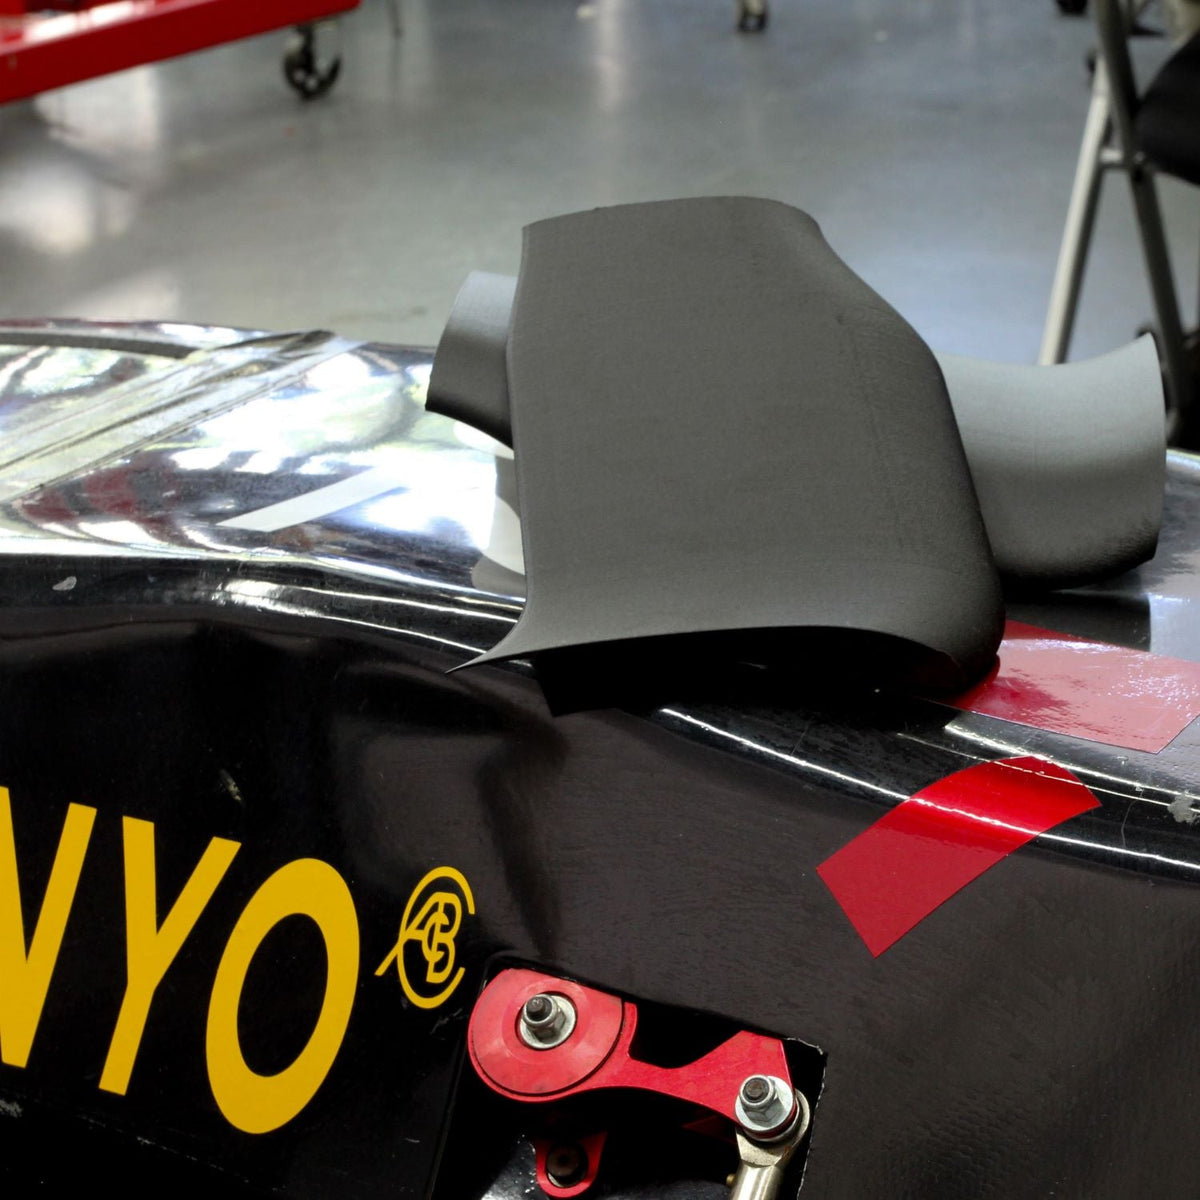
Perfect for automotive, aerospace, robotics, and industrial parts where strength, durability, and precision are essential.
Choose Fiberon™ PET-CF17 for your engineering projects when you need a composite material that combines high strength, heat resistance, moisture insensitivity, and reliable, easy printing.
Printing Requirements
- All-metal hotend 270˚C+
- Hardened nozzle
- Annealing post printing
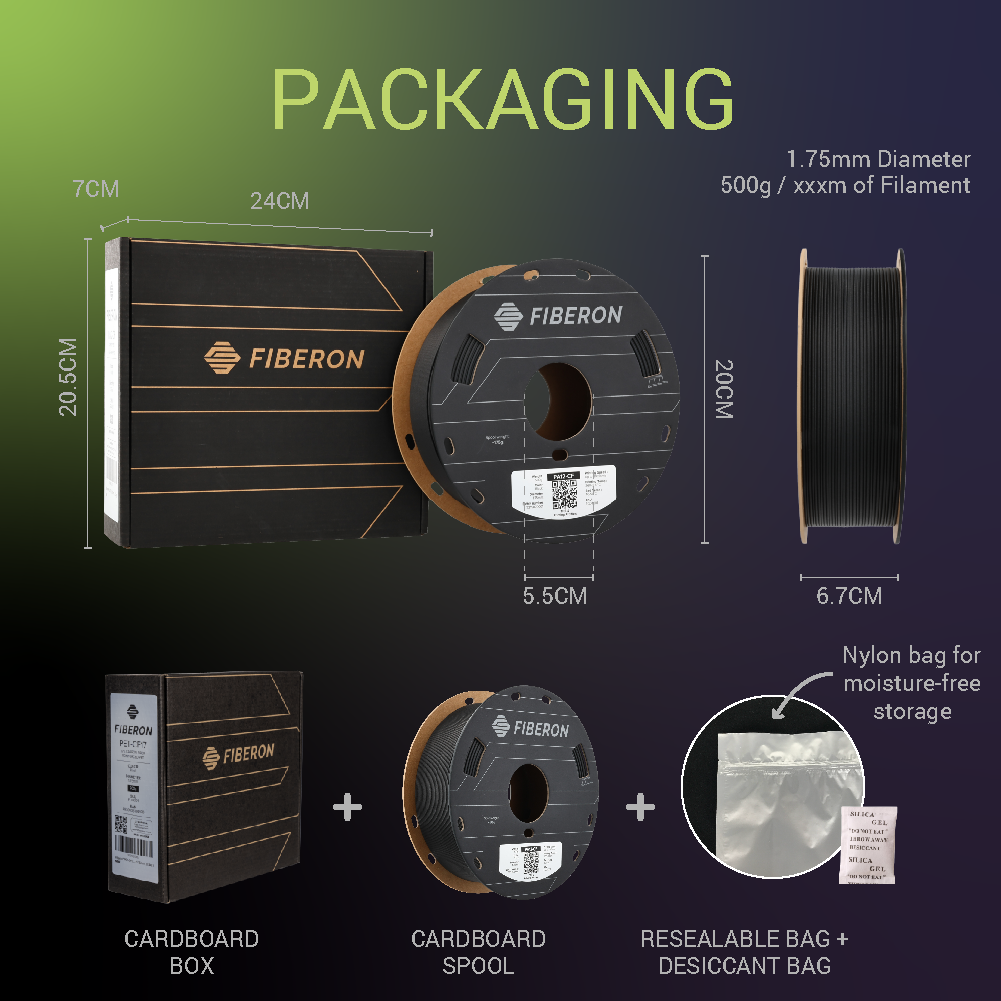
- You may need a filament dryer (such as the PolyDryer) depending on the humidity of your environment. Keep dry when not in use.
Printing Tips
- Use an all-metal hotend within 270-300°C and a wear-resistant nozzle because the carbon-fiber reinforcement is abrasive.
- Dry at 100°C for 10 hours and keep the filament dry during use.
- An enclosed printer is recommended; keep the chamber door closed during printing.
- For the annealed performance stated in the TDS, anneal at 120°C for 10 hours.
- Before annealing, allow the print to rest for more than 24 hours or place it at 80°C for 2 hours; do not apply load and keep the oven temperature uniform.
- Retain supports for bridges or overhangs and reinforce thin walls when deformation is a concern.
Print Settings
Printing Temperature: 270˚C - 300˚C
Build Plate Temperature: 70˚C - 80˚C
Chamber Temperature: Room Temperature
Printing Speed: up to 300mm/s
Cooling Fan: OFF
Compatibility: 0.4mm+ hardened nozzle required
Direct Drive:
Retraction Distance: 3mm
Retraction Speed: 40mm/s
Indirect Drive:
Retraction Distance: 6mm
Retraction Speed: 60mm/s
Recommended Drying Settings
Regular Oven: 100˚C for 10h
PolyDryer: Level 3 for 18h
(Only if the material has absorbed moisture)
Annealing Settings
120˚C for 10h
For Parts With Large Overhangs or Thin Sections: 100˚C for 14h
Certifications
REACH | RoHS | 889 | PCP | ISO9001 CERT | PROP65WARNING


