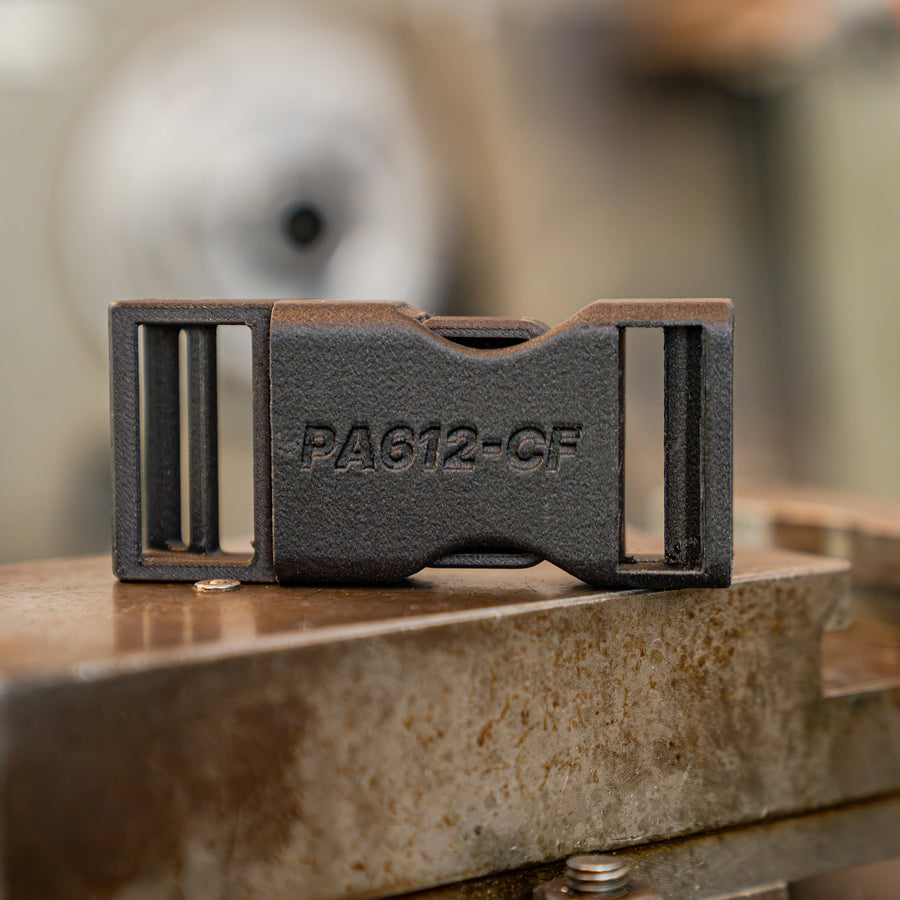
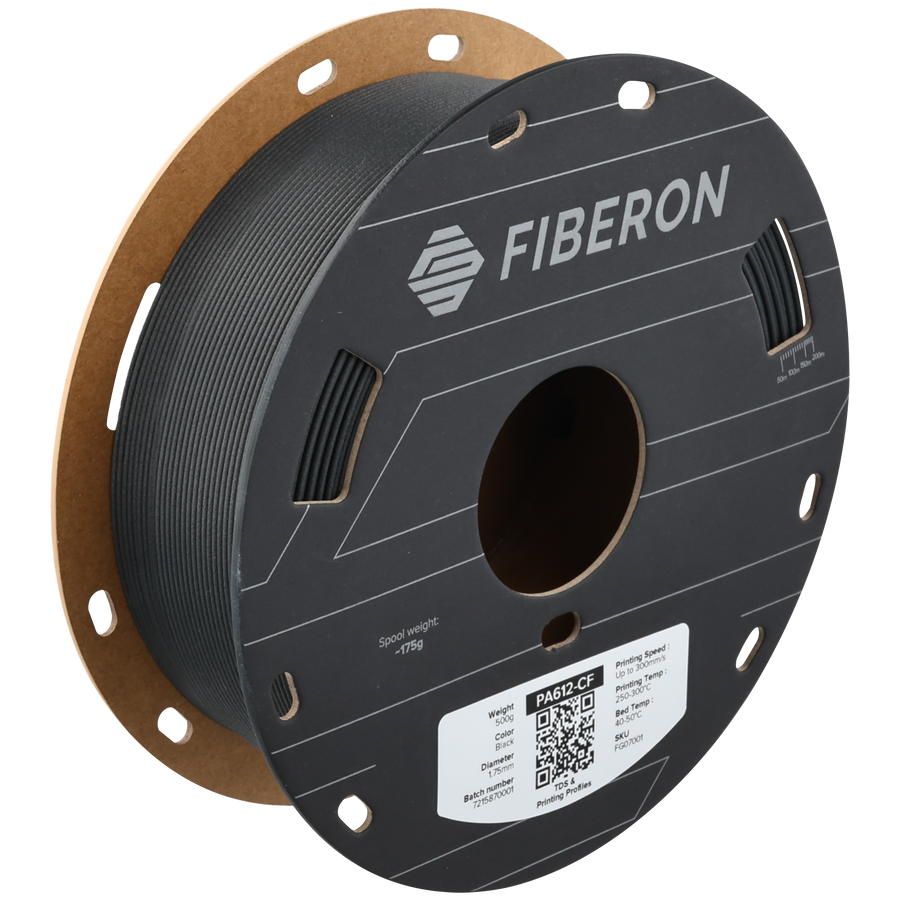


Description
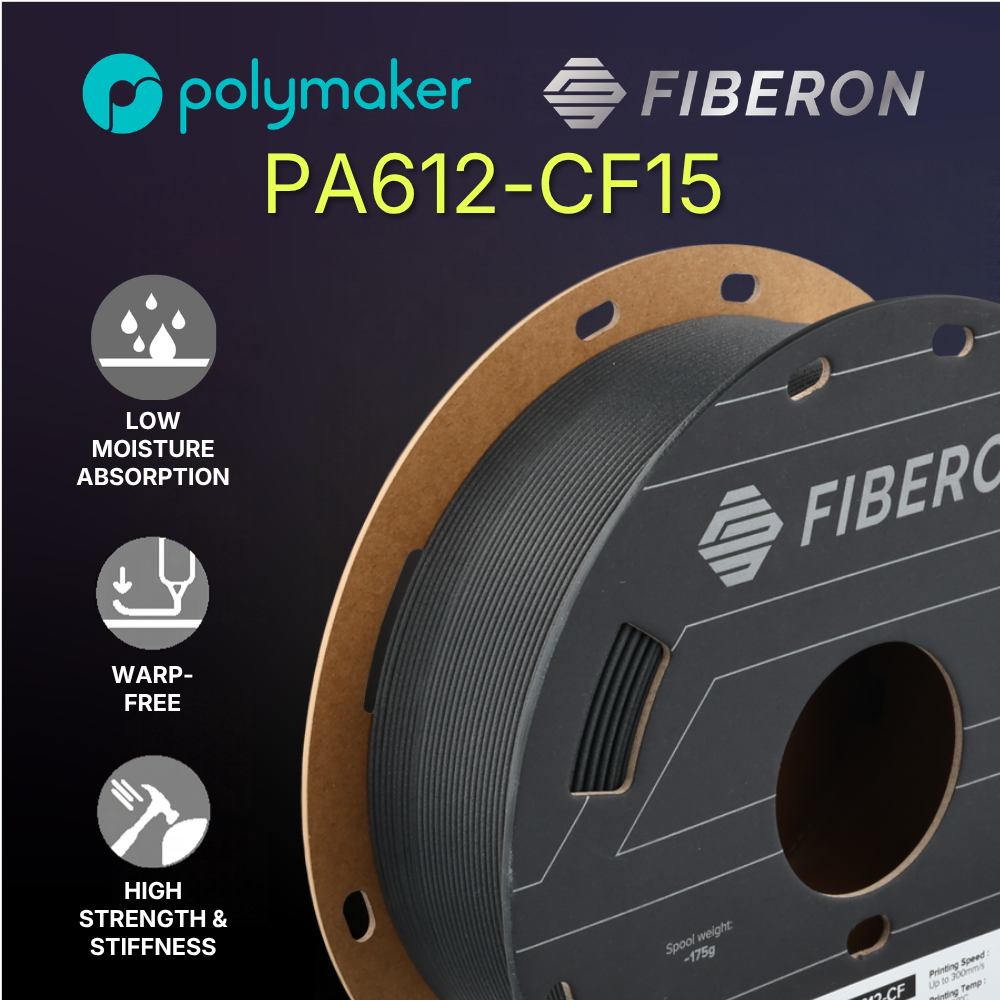
✓ Lower Moisture Absorption Than PA6
✓ High Strength & Stiffness
✓ Carbon Fiber Reinforced
✓ Warp-free Technology
✓ Ready to Print
Fiberon™ PA612-CF15: Advanced Carbon Fiber Reinforced PA612 Filament
Superior Engineering Performance (Formerly PolyMide™ PA612-CF)
Fiberon™ PA612-CF15 is a carbon fiber reinforced long-chain copolyamide (PA612) filament designed for high-performance engineering applications. Its unique chemical structure results in significantly lower moisture sensitivity than traditional PA6/66 and PA6-based nylons, while offering better mechanical properties than PA12-based materials.
Key Features and Advantages
✓ Low Moisture Sensitivity: Maintains dimensional accuracy and mechanical strength, even in humid environments, reducing the need for frequent drying.
✓ Enhanced Mechanical Properties: Outperforms PA12-based filaments in tensile strength, stiffness, and durability, making it ideal for demanding functional parts.
✓ Carbon Fiber Reinforcement: 15% carbon fiber content delivers excellent rigidity, high strength, and improved thermal stability.
✓ Warpfree™ Technology: Proprietary formulation minimizes warping and enhances print size stability, even on large or complex parts.
✓ Consistent Quality: Fiberon™ PA612-CF15 is the same trusted formula as PolyMide™ PA612-CF, though it may print in a slightly darker black shade.
Ideal for Industrial and Engineering Applications
Perfect for automotive, aerospace, robotics, jigs, fixtures, and end-use components where dimensional stability, moisture resistance, and mechanical performance are critical.
Choose Fiberon™ PA612-CF15 for your most demanding projects when you need a carbon fiber nylon that combines low moisture sensitivity, superior mechanical properties, and exceptional print reliability.
Fiberon™ PA612-CF15 is the same great formula as PolyMide PA612-CF, although Fiberon™ PA612-CF15 may print in a slightly darker black shade color than its predecessor.
Printing Requirements
• All-metal hotend 250˚C+ recommended
• Hardened nozzle
• Filament dryer (e.g. PolyDryer)
• Annealing post printing
• Moisture conditioning after Annealing
Printing Tips
• Use a wear-resistant nozzle, such as hardened steel or ruby, because the carbon-fiber reinforcement is abrasive.
• Store and print under dry conditions (relative humidity below 20%); dry at 100°C for 10 hours before use.
• Use a 40-50°C build plate, and turn the cooling fan OFF; an actively heated chamber is not required.
• Use glue stick or Magigoo PA if bed adhesion is weak.
• If the material is used as its own support, remove the support before excessive moisture absorption to avoid permanent bonding.
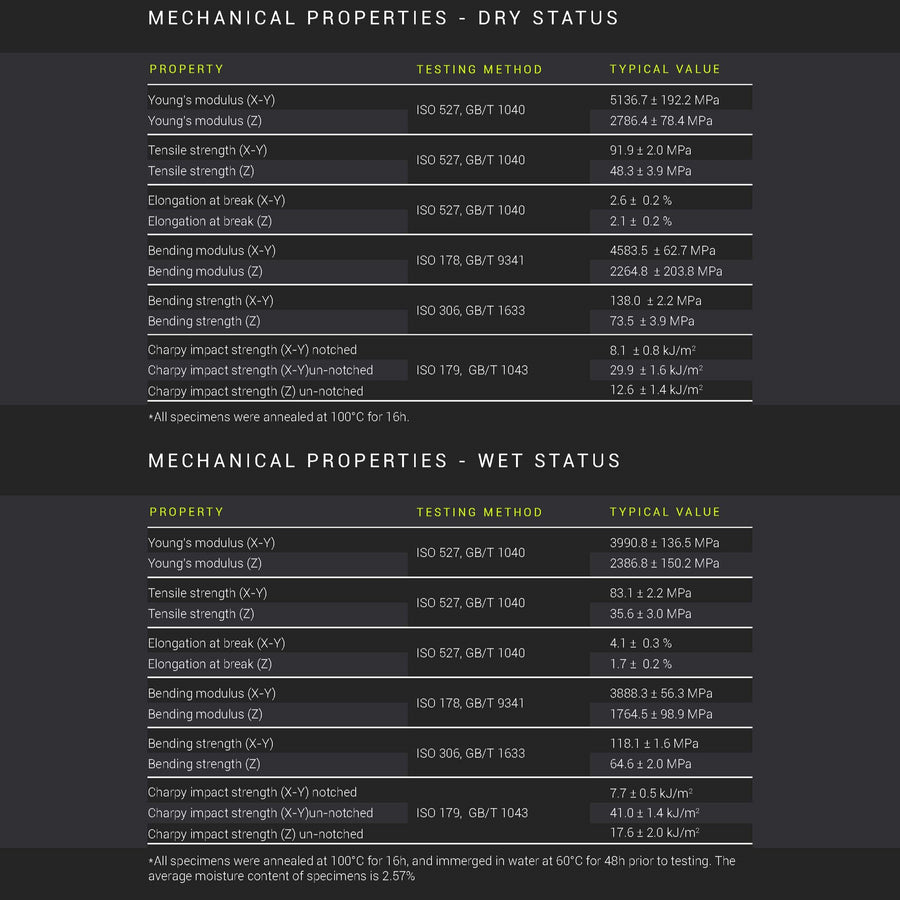
• Anneal at 100°C for 16 hours when the annealed performance stated in the TDS is required.
Print Settings
Printing Temperature: 250˚C - 300˚C
Build Plate Temperature: 40˚C - 50˚C
Chamber Temperature: Room Temperature
Printing Speed: up to 300mm/s
Cooling Fan: OFF
Direct Drive:
Retraction Distance: 3mm
Retraction Speed: 40mm/s
Indirect Drive:
Retraction Distance: 6mm
Retraction Speed: 60mm/s
Recommended Drying Settings
Regular Oven: 100˚C for 10h
PolyDryer™: Level 3 for 18h
(Only if the material has absorbed moisture)
Annealing Settings
100˚C for 16h
Certifications
REACH | RoHS | 889 | PCP | ISO9001 CERT | PROP65WARNING


