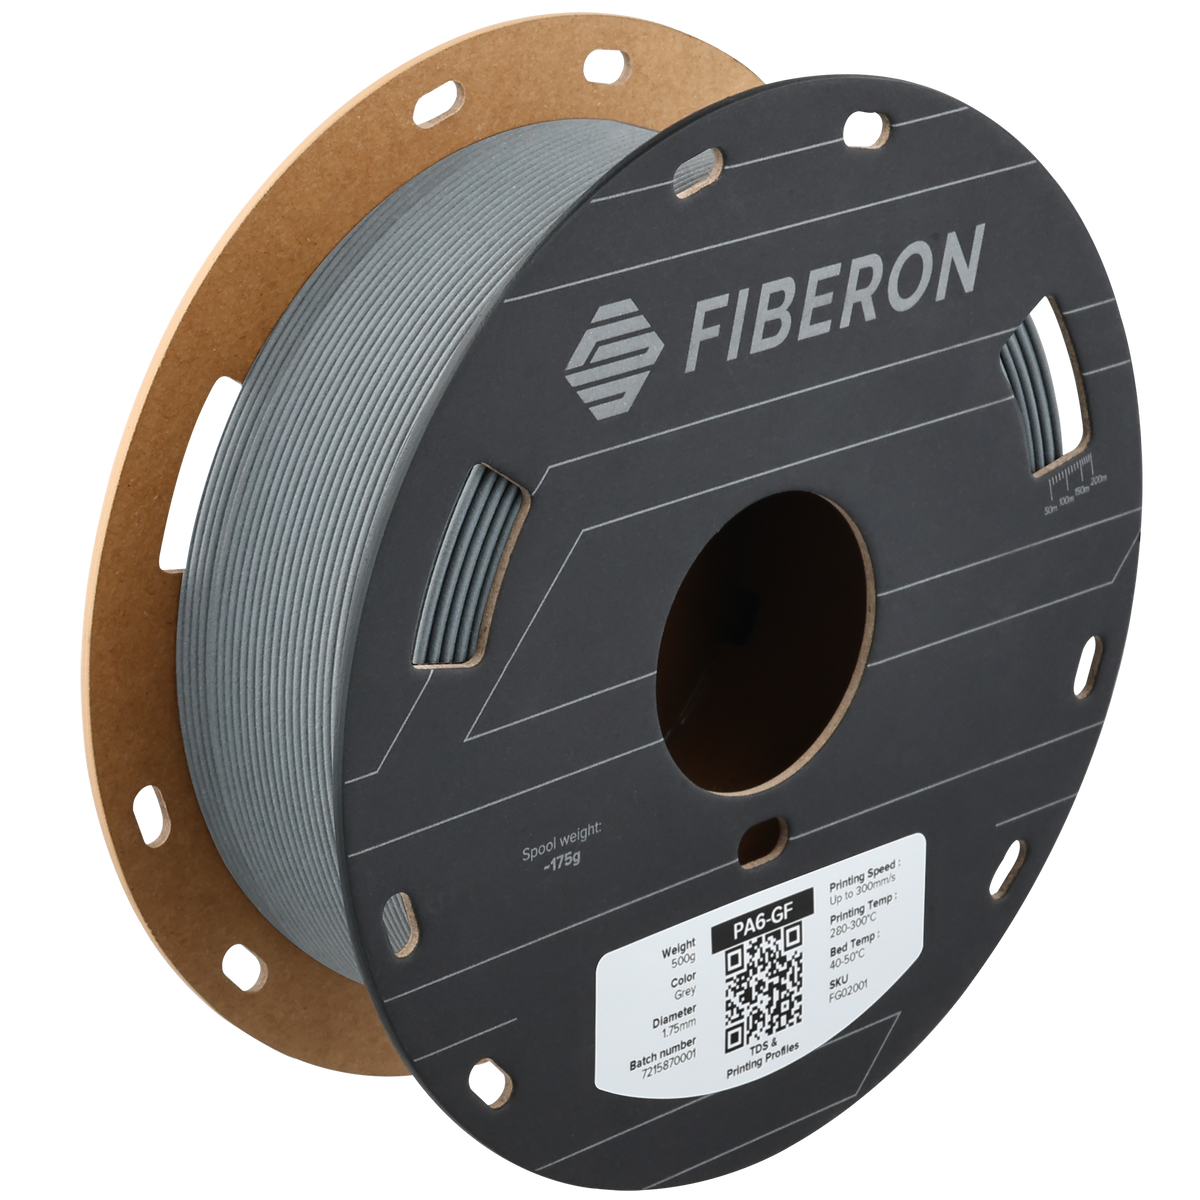


Description
✓ High Strength & Stiffness
✓ High Heat Resistance
✓ Highest Layer Adhesion
✓ Warp-Free™ Technology
✓ High-Speed Printing
Fiberon™ PA6-GF25: High-Performance Glass Fiber Reinforced Nylon 6 Filament (Formerly PolyMide™ PA6-GF)
Exceptional Strength, Stiffness, and Heat Resistance
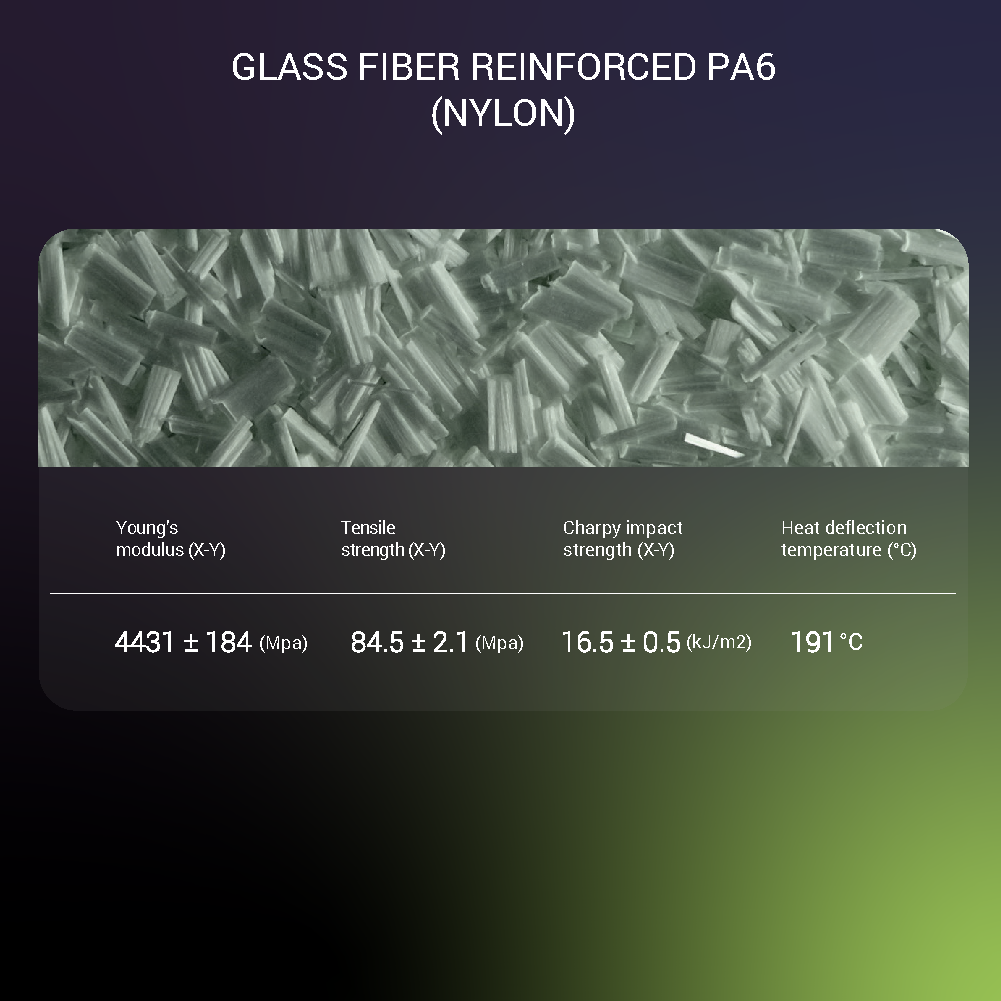
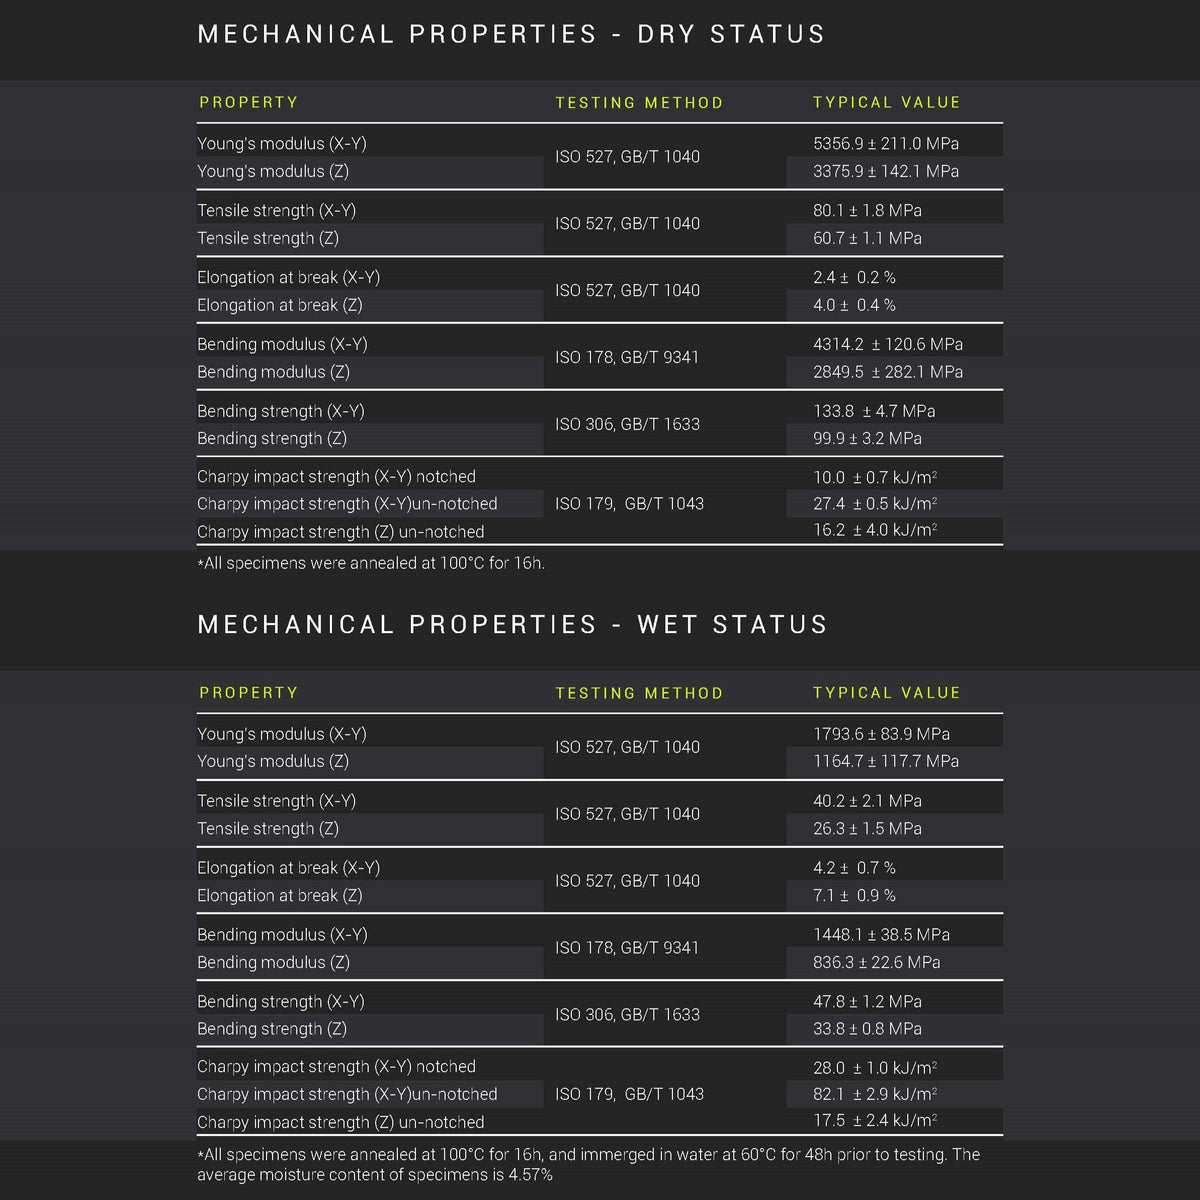
Fiberon™ PA6-GF25 is a glass fiber reinforced PA6 (Nylon 6) filament containing 25% glass fiber by weight. This advanced composite material delivers outstanding mechanical strength, high stiffness, and excellent thermal properties, making it ideal for demanding engineering, automotive, aerospace, and industrial applications.
Key Features
- 25% Glass Fiber Reinforcement: Significantly enhances rigidity, strength, and dimensional stability.
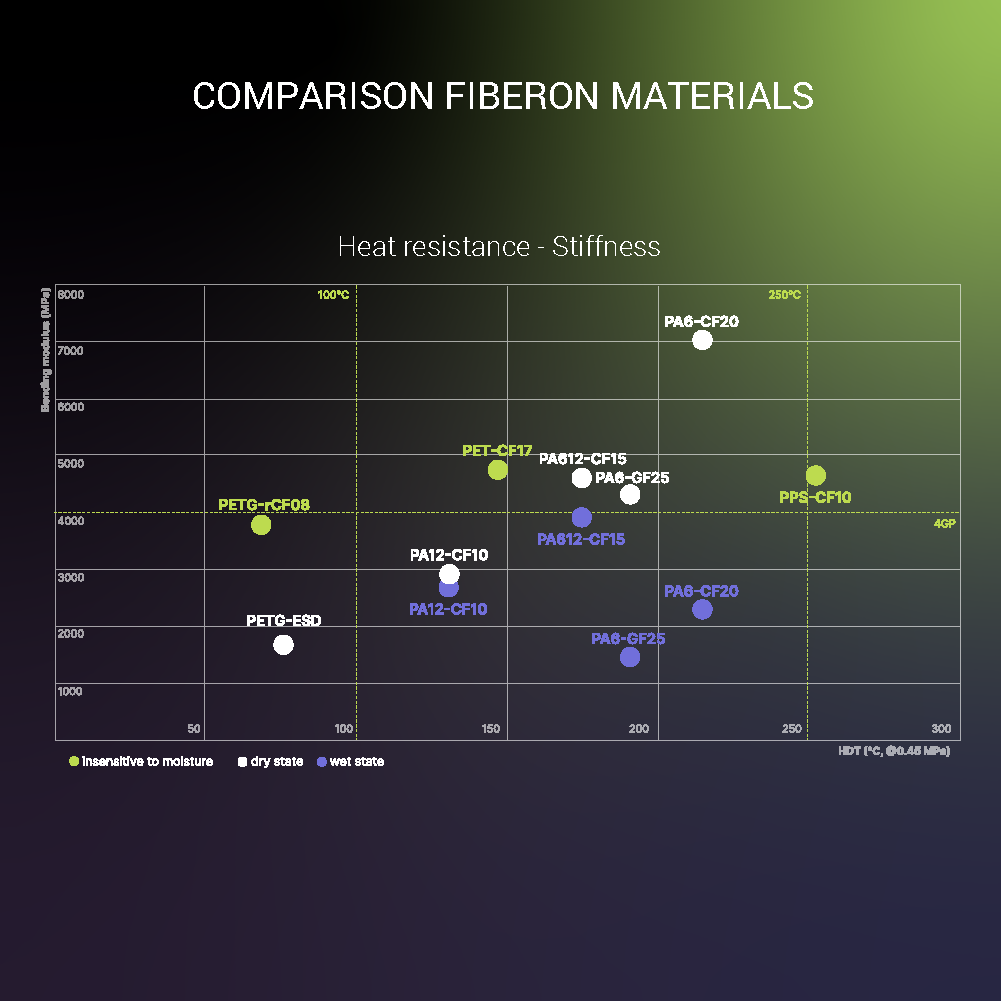
- Excellent Thermal Properties: Withstands high temperatures, featuring a heat deflection temperature (HDT) of up to 191°C after annealing.
- Superior Layer Adhesion: Maintains strong interlayer bonding for durable, cohesive prints.
- Minimal Warping: Warp-Free™ technology allows printing at lower bed temperatures (40–50°C), reducing the risk of warpage and improving dimensional accuracy.
- High-Speed Printing: Compatible with print speeds up to 300 mm/s.
Easy-to-Use for Advanced Users
Fiberon™ PA6-GF25 does not require a heated chamber and can be printed reliably on high-performance FDM/FFF 3D printers equipped with a hardened steel nozzle due to the abrasive nature of glass fibers. For best results, filament drying before printing and post-print annealing (100°C for 10–16 hours) are strongly recommended to maximize mechanical and thermal performance.
Same Trusted Formula, New Name
Fiberon™ PA6-GF25 is the same high-performance material as PolyMide™ PA6-GF, now under the Fiberon™ brand.
Choose Fiberon™ PA6-GF25 for applications requiring maximum strength, stiffness, and heat resistance without compromising printability or layer adhesion.
Formerly called PolyMide PA6-GF.
Printing Requirements
- All-metal hotend 280°C+
- Hardened nozzle
- Filament dryer (we recommend the PolyDryer)
- Annealing post printing
- Moisture conditioning after annealing
Printing Tips
- Use a wear-resistant nozzle, such as hardened steel or ruby, because the glass-fiber reinforcement is abrasive.
- Store and print under dry conditions (relative humidity below 20%); dry at 100°C for 10 hours before use.
- Use a 40-50°C build plate, and turn the cooling fan OFF; an actively heated chamber is not required.
- Use glue stick or Magigoo PA if bed adhesion is weak.
- If the material is used as its own support, remove the support before excessive moisture absorption to avoid permanent bonding.
- Anneal at 100°C for 16 hours when the annealed performance stated in the TDS is required.
Print Settings
- Printing Temperature: 280°C - 300°C
- Build Plate Temperature: 40°C - 50°C
- Chamber Temperature: Room Temperature
- Printing Speed: up to 300mm/s
- Cooling Fan: OFF
- Direct Drive: Retraction Distance 3mm, Retraction Speed 40mm/s
- Indirect Drive: Retraction Distance 6mm, Retraction Speed 60mm/s
Recommended Drying Settings (only if the material has absorbed moisture)
- Regular Oven: 100°C for 10h
- PolyDryer: Level 3 for 18h
Annealing Settings: 100°C for 16h
Certifications
REACH | RoHS | 889 | PCP | ISO9001 CERT | PROP65WARNING


