



Description
✓ High Strength & Stiffness
✓ High Heat Resistance
✓ Easy to Print
✓ Low Warping
✓ Ready to Print
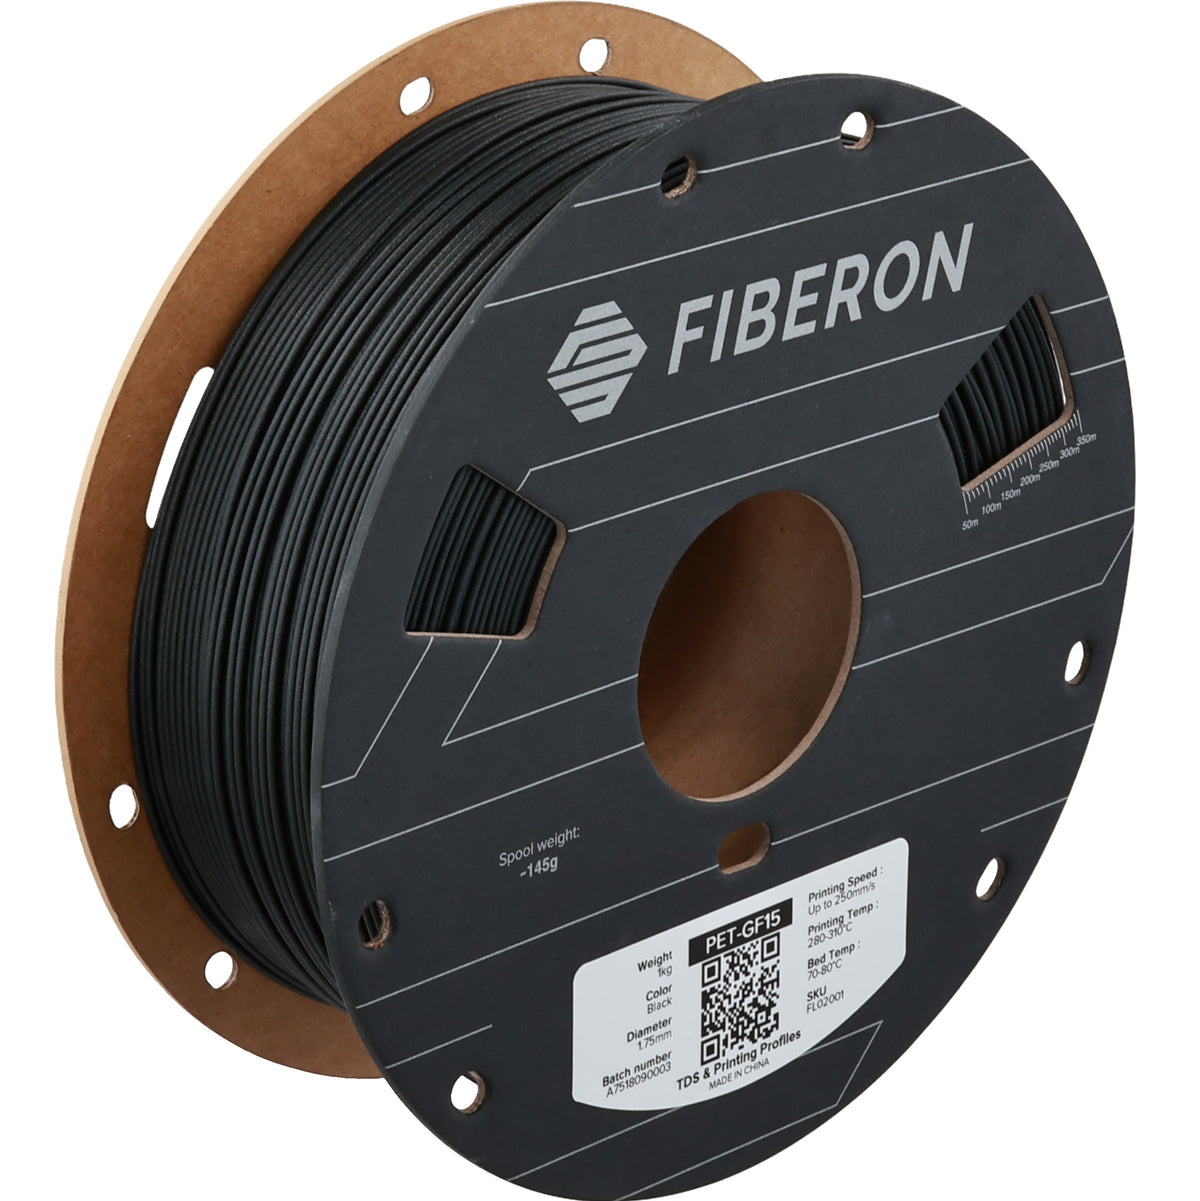
Fiberon™ PET-GF15 – Glass-Fiber-Reinforced PET Filament
Bridge the gap between everyday usability and industrial performance.
- High-Strength, Heat-Resistant Engineering Filament
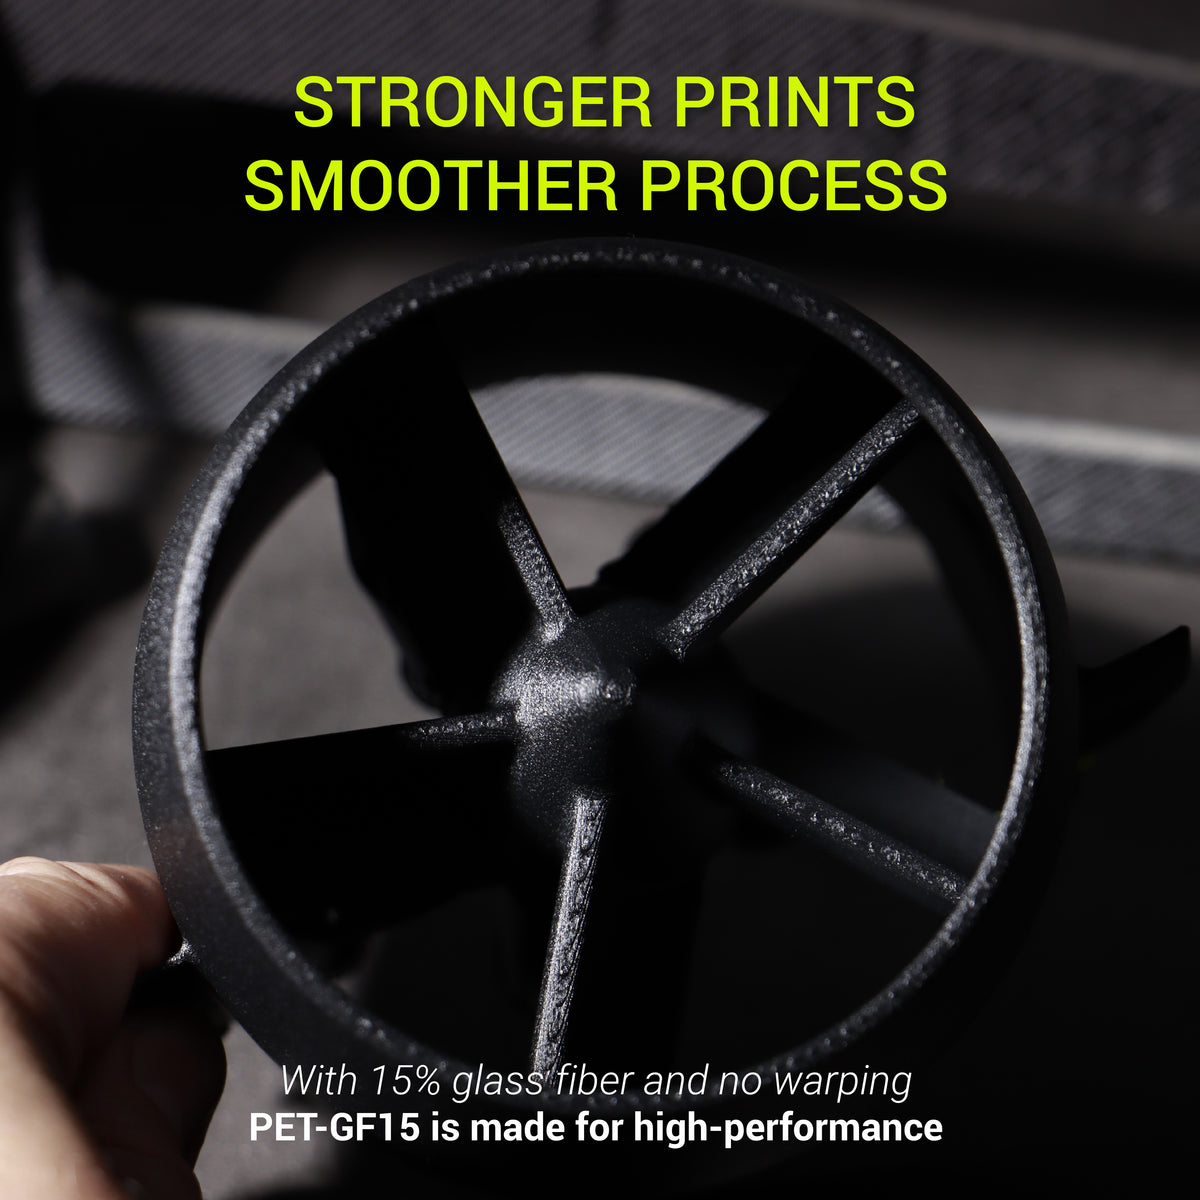
Fiberon™ PET-GF15 combines PET with 15% glass fiber reinforcement to deliver exceptional stiffness, dimensional stability, and thermal resistance. It’s engineered for users who need the toughness of an engineering-grade filament without sacrificing printability.
- Industrial-Level Performance, Everyday Usability
With a bending strength of 104 MPa and HDT up to 133 °C (0.45MPa, after annealing), PET-GF15 withstands high stress and high-temperature environments where other materials would deform. It prints easily on most modern FDM printers, even at speeds up to 250 mm/s.
- Excellent Surface Finish & AMS Compatible
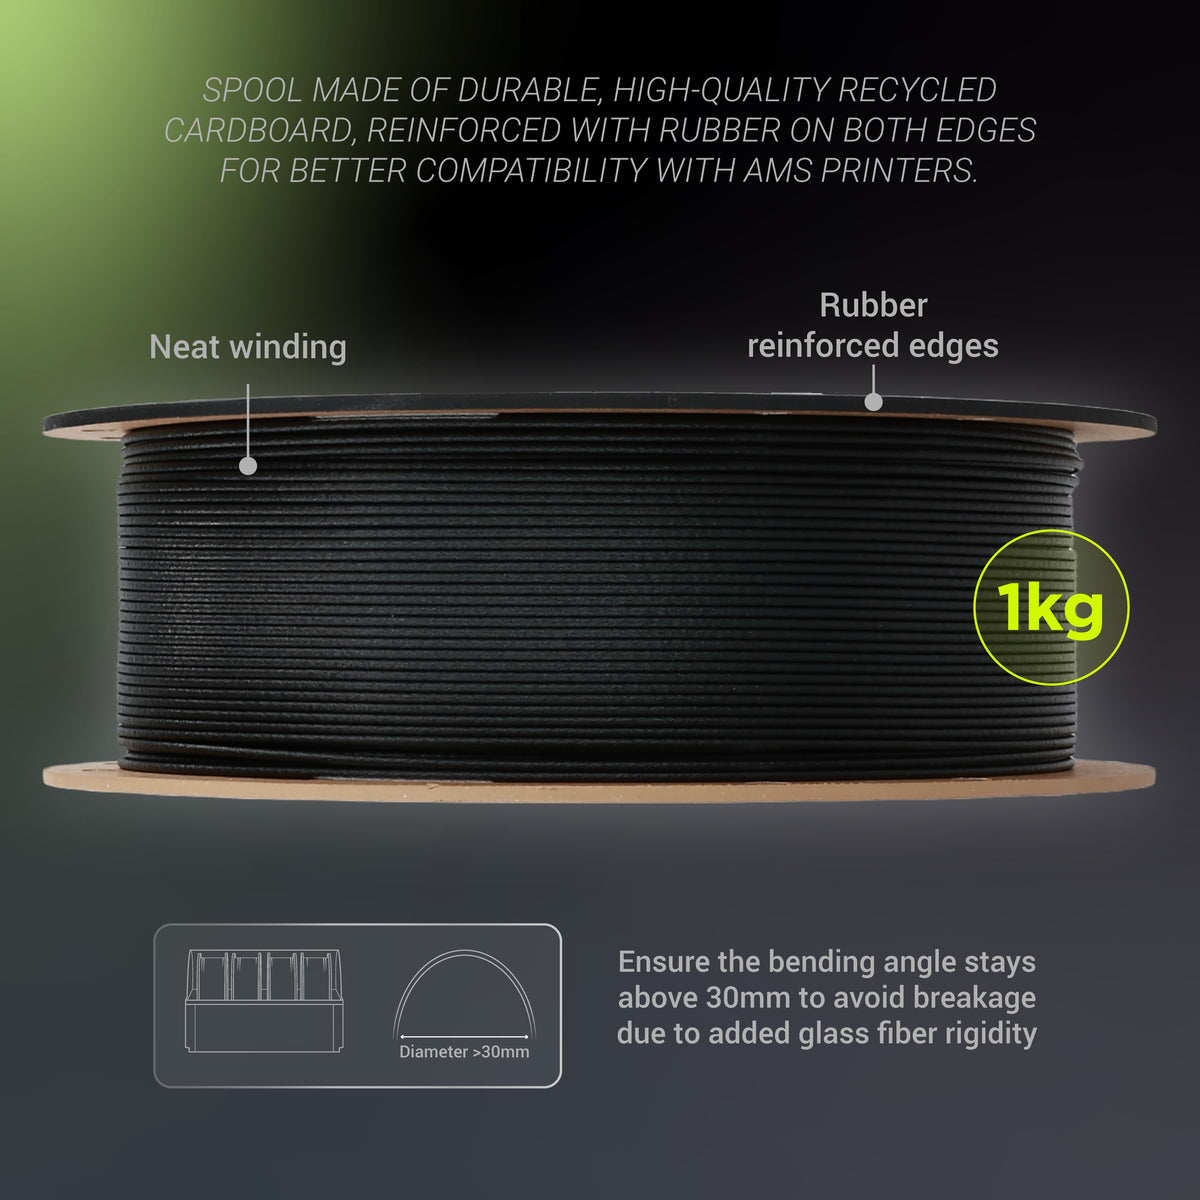
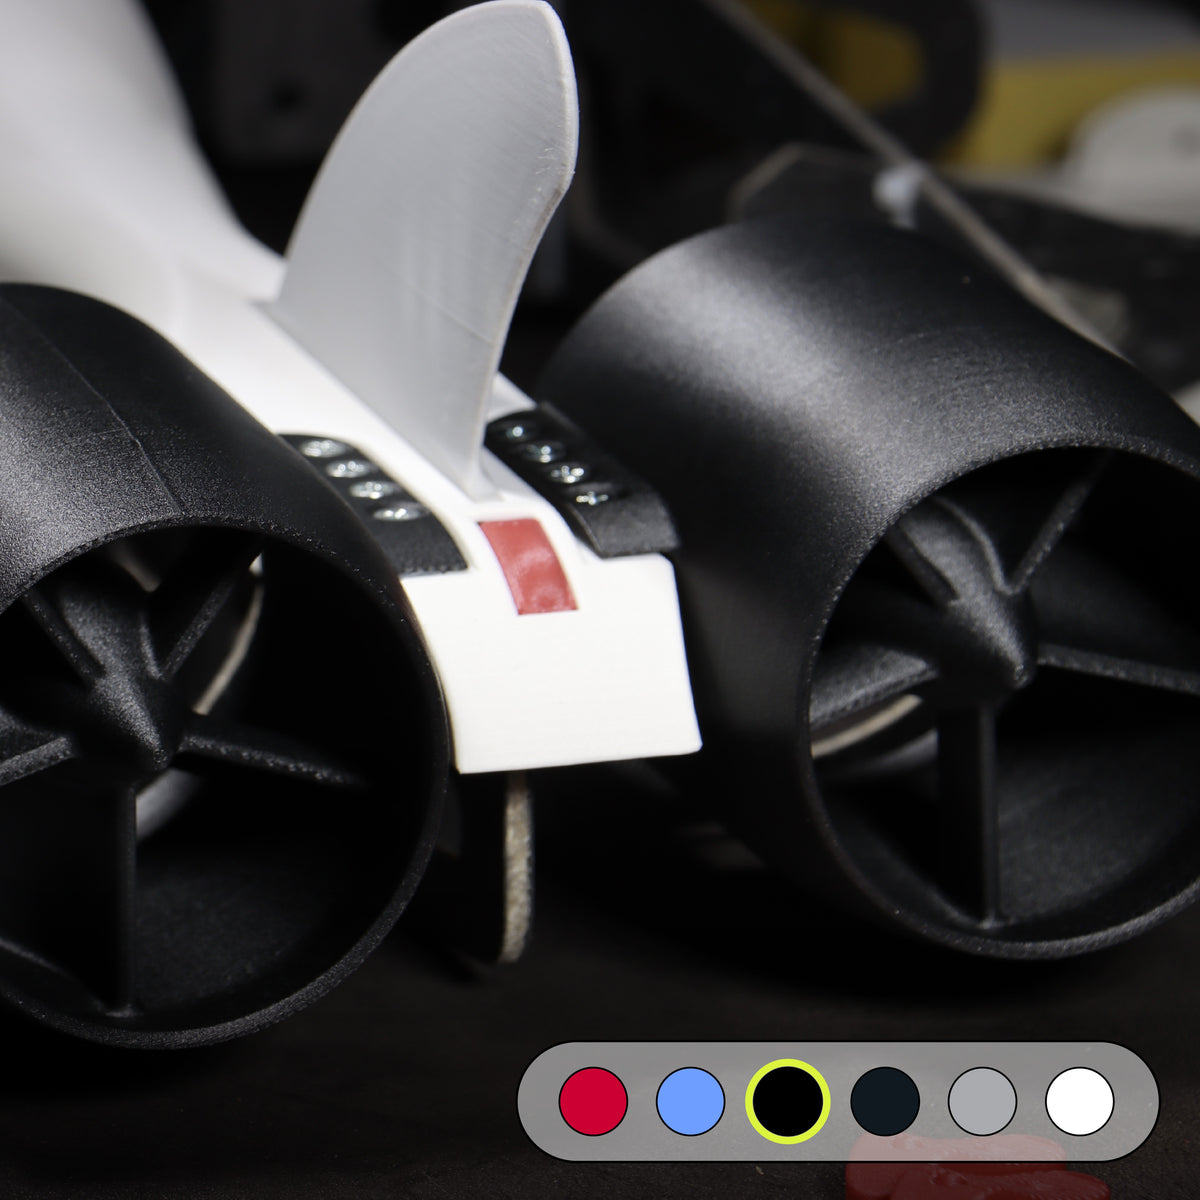
Achieve smooth, professional-grade prints with a refined texture that minimizes visible layer lines. Fiberon™ PET-GF15 works seamlessly with most multi-material systems, perfect for multi-color and multi-material projects.
- Dimensional Stability & Low Warping
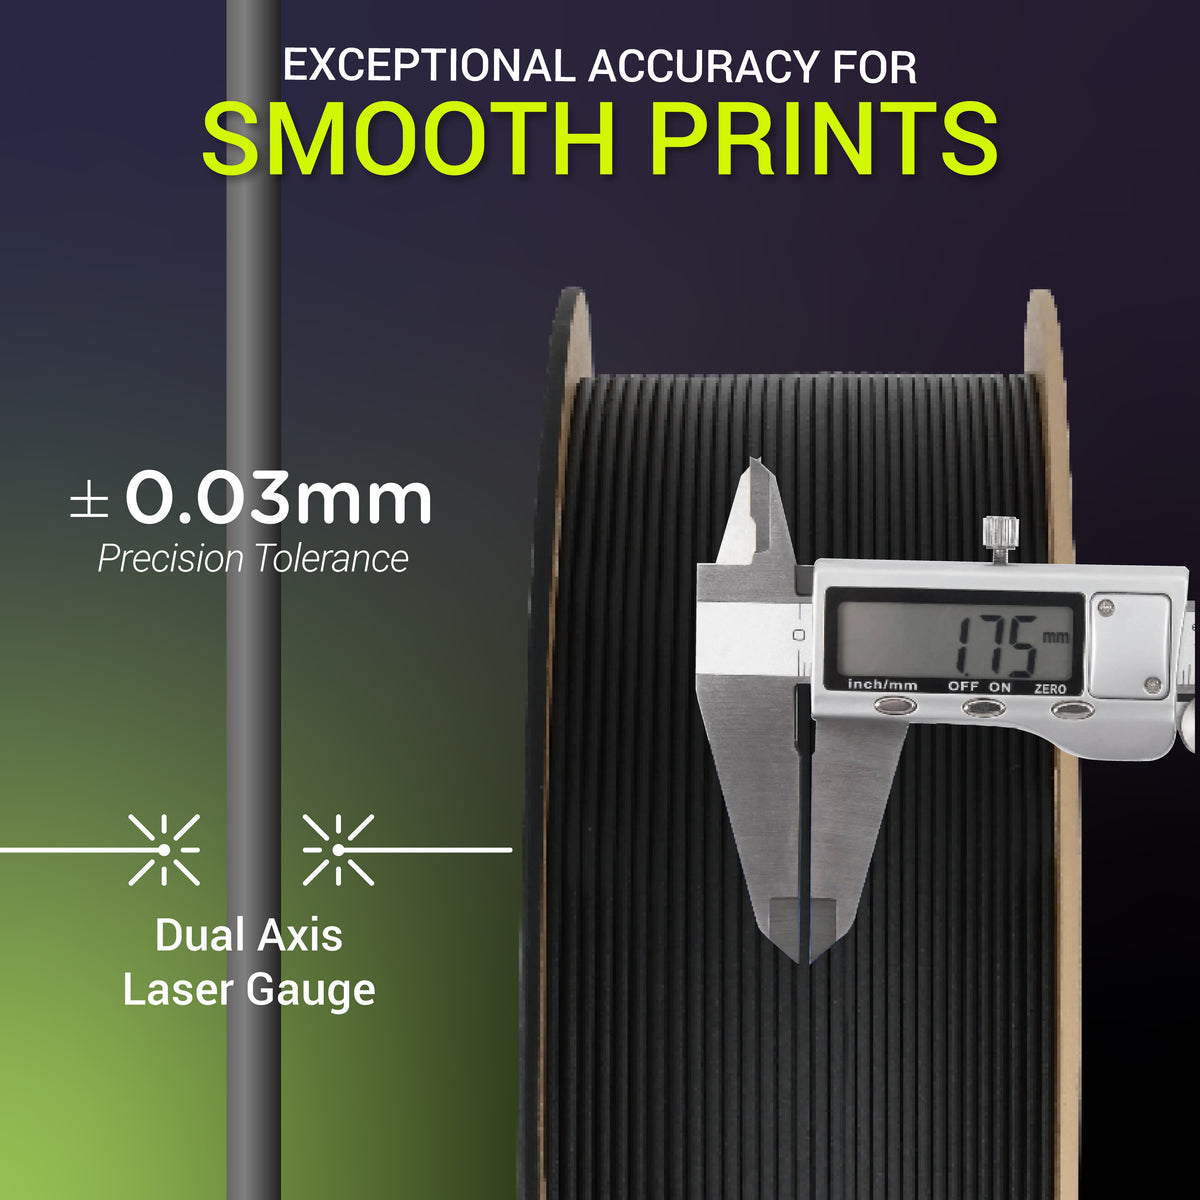
PET-GF15 maintains consistent accuracy and minimal warping, even on large projects. After annealing, dimensional change stays below 0.5 %, ensuring tight tolerances for functional parts that demand reliability and precision.
- Designed for Professionals & Makers Alike
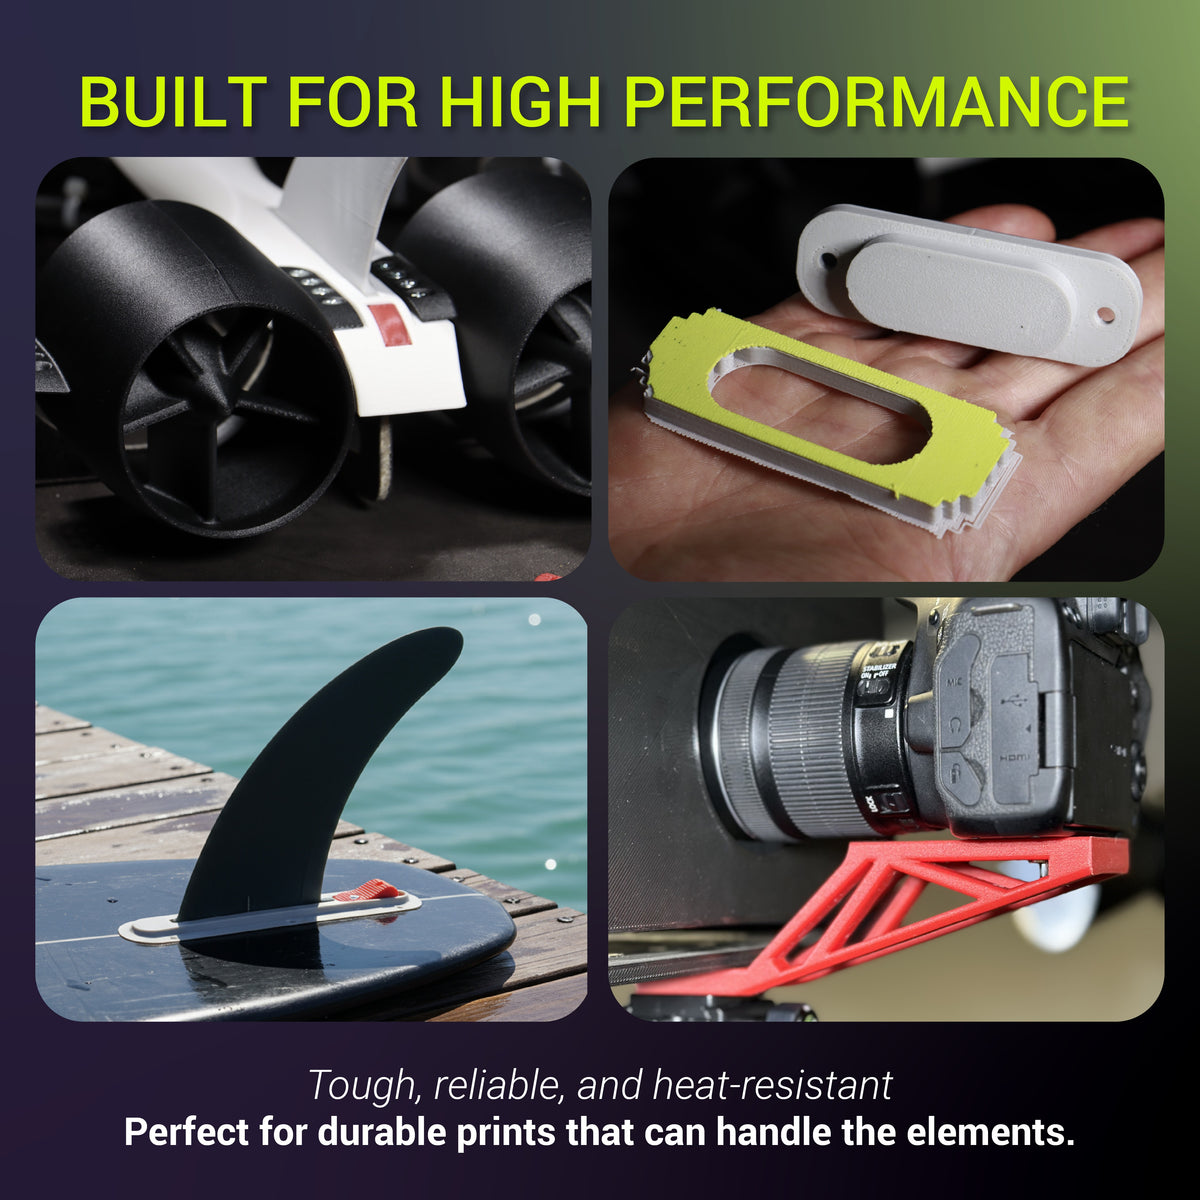
Ideal for automotive parts, jigs, fixtures, industrial parts, and prototyping, PET-GF15 offers excellent toughness and resists brittleness. Whether you’re a professional engineer or advanced hobbyist, PET-GF15 delivers industrial-grade results with a user-friendly experience.
Warning: PET-GF filament adheres strongly to textured PEI plates—allow plate to cool before removal or use a release agent to prevent damage.
Printing Tips
- Use a wear-resistant nozzle, such as hardened steel or ruby; brass-nozzle life may be approximately 9 hours.
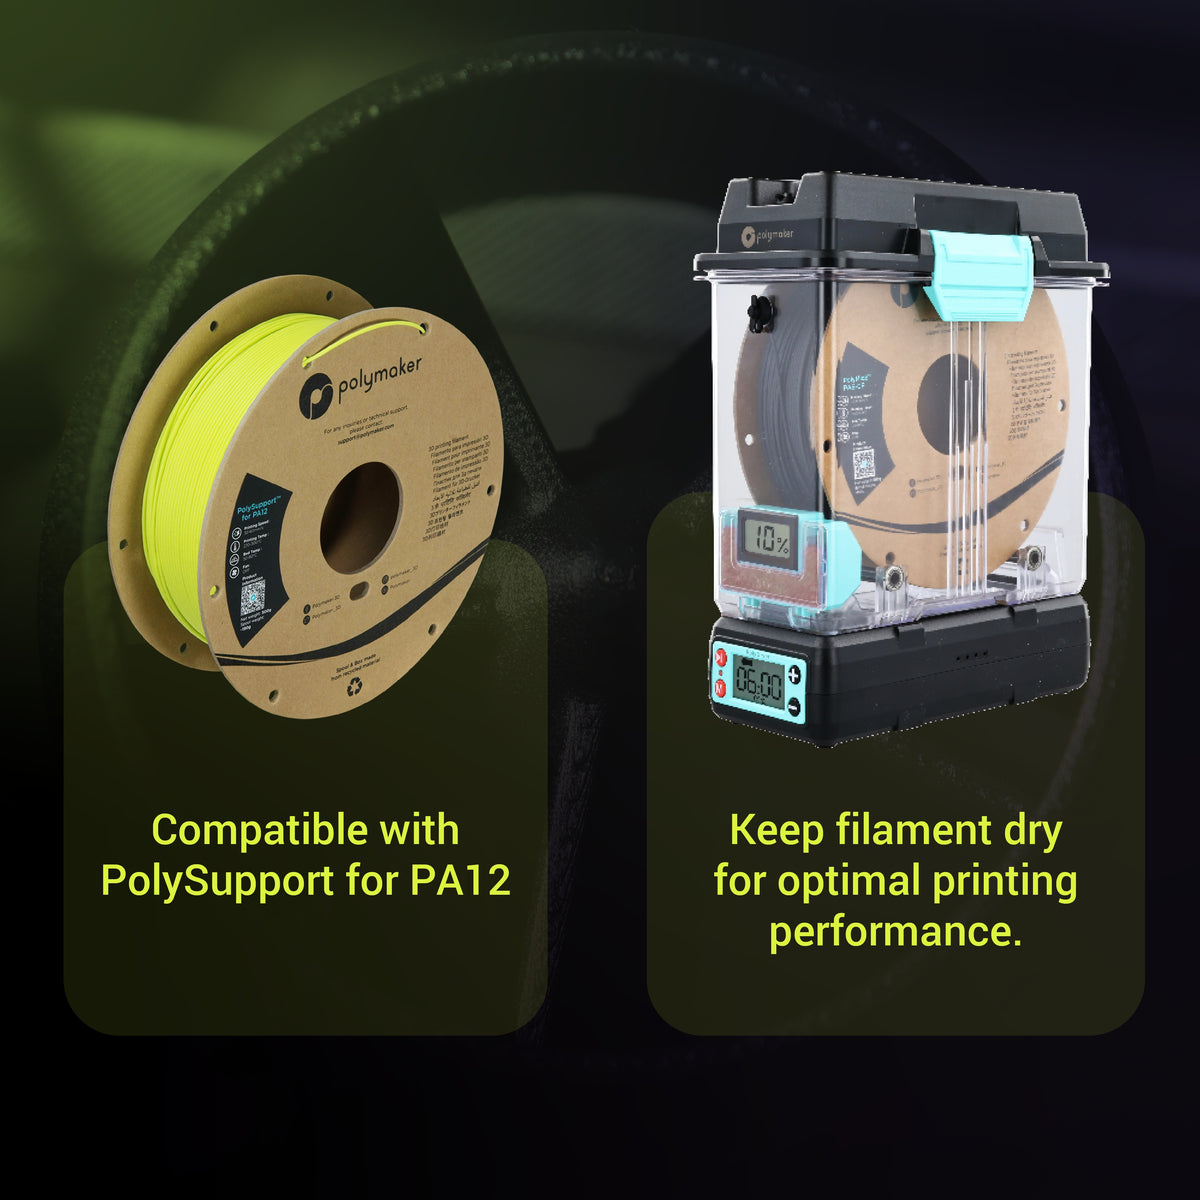
- Store and print under dry conditions (relative humidity below 20%); dry at 100°C for 10 hours before use. The Polymaker PolyDryer is ideal for this.
- An enclosed printer is recommended; keep the chamber door closed during printing.
- Use glue as a release layer on textured PEI and wait until the build plate reaches room temperature before removing the print.
- Anneal at 120°C for 16 hours for the best heat resistance and mechanical performance.
- During annealing, avoid applied loads and non-uniform oven temperature, and retain supports where needed to limit deformation.
Print Settings
Printing Temperature: 280°C - 310°C
Bed Temperature: 70°C - 80°C
Printing Speed: up to 250mm/s
Enclosure: Recommended
Drying Settings: 100°C for 10h
Compatibility: 0.4mm+ hardened nozzle required
Certifications
REACH | RoHS | 889 | PCP | ISO9001 CERT | PROP65WARNING


